

精密機械加工

精密機械加工
設計から、素材調達、加工、組立、検査、洗浄、梱包出荷まで最先端の技術による一貫したものづくりが可能です。 半導体業界の厳しい要求に対応し、培ってきた技術力による高精度な金属加工を実現します。 当社独自の精密研磨と精密洗浄の技術により、平滑で高清浄な表面を得る事ができます。 樹脂加工は温度、湿度管理されたクリーンルームで切削加工することにより金属加工品と同等の寸法精度で加工します。 最終洗浄からパッケージングまでクリーンルームで対応可能です。
1~14 item / All 14 items
-
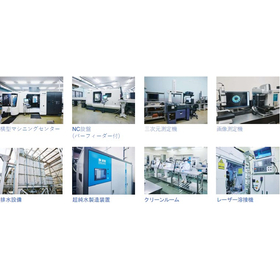
Kanekita Corporation Company Profile
We have a long history in metal processing, starting with stainless steel!
last updated
-

Stainless steel "SUS316L-K material, KVA material"
It has excellent corrosion resistance and weldability, achieving high cleanliness!
last updated
-

Resin processing
By processing in a clean room, we achieve dimensional accuracy comparable to that of metal products!
last updated
-

Composite Electrolytic Polishing
After precision grinding, electro-polishing is performed to achieve a high-purity surface!
last updated
-

Cleaning
We perform cleaning using pure water and ultra-pure water to achieve the cleanliness desired by our customers!
last updated
-

Metal processing
We respond to complex shapes and various sizes with advanced technology and state-of-the-art equipment!
last updated
-

Kanekita Corporation Owned Equipment
We are constantly introducing advanced processing machines to achieve a reduction in manufacturing costs!
last updated
-

Inactivation processing
A treatment that modifies the surface material, different from coatings such as plating aimed at rust prevention!
last updated
-

Welding
We use different methods such as fiber laser welding according to the material and application!
last updated
-
[Proposal Example] Materials and Surface Treatment for Reducing Vacuum Arrival Time
Reduced vacuum arrival time by approximately 20%! A case study proposing materials and surface treatments.
last updated
-
[Proposal Example] Addressing Cost and Delivery Challenges with Materials and Surface Treatment
Achieved a target Ra of 0.4 or lower with cutting processing and electro polishing! A case study that reduced polishing costs by approximately 50%.
last updated
-
[Example Proposal] Surface Treatment for Improved Work Efficiency
Solve the problem of the nozzle getting caught at the joint with surface treatment! Contributes to approximately 15% time reduction.
last updated
-
[Proposal Example] Problem Solving through Changes in Welding Methods
Proposed changes in welding and cleaning to address concerns about weld penetration and burn-through, resulting in a total reduction of approximately 30% in man-hours.
last updated
-
[Proposal Example] Material Change
Improvement by changing the material of equipment parts with high wear frequency! Contributed to approximately 40% reduction in man-hours.
last updated